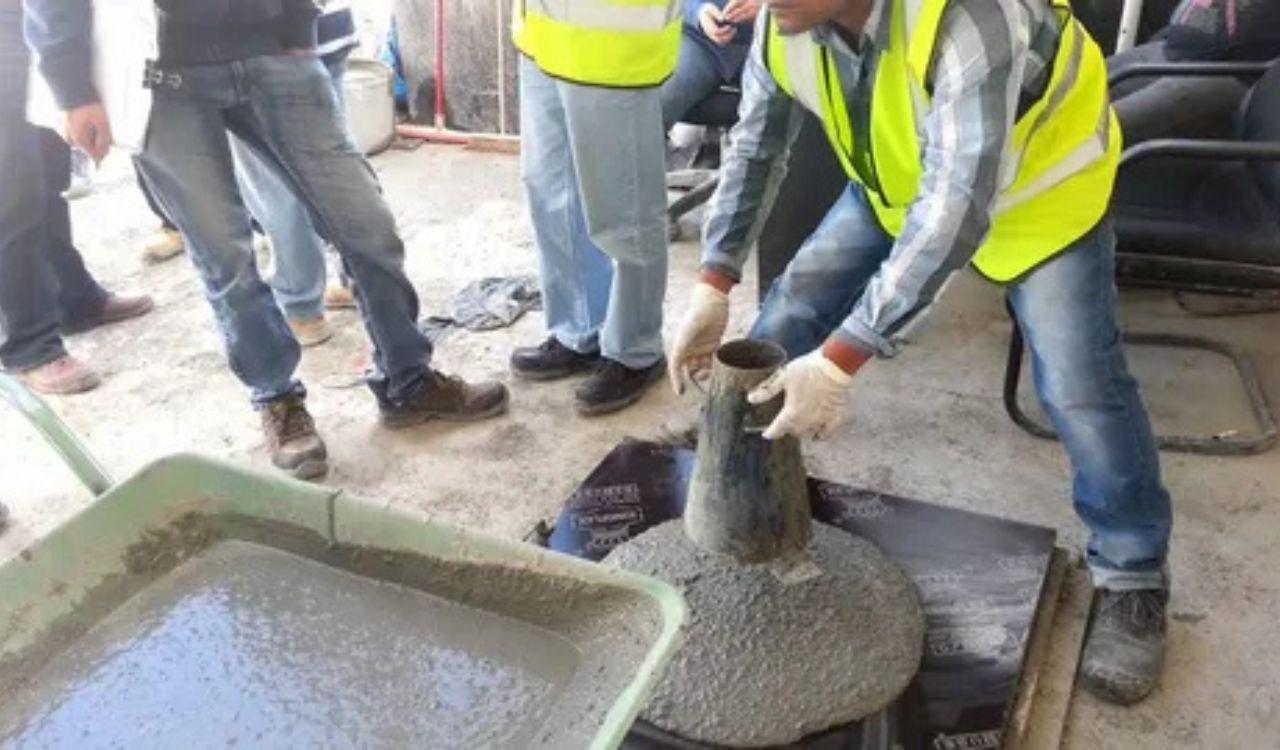
A mix that behaved perfectly yesterday suddenly stiffens within minutes today. Nothing changed in the mix design, the admixture dose looks right, and the aggregates test normal. The one thing that did change is the cement, which arrived hot from the mill or silo.
Fresh-from-mill hot cement can cause sudden slump loss in concrete through two routes. It changes the form of calcium sulfate that controls early hydration and adds heat directly to the mix. This article explains both mechanisms, how to distinguish them from ordinary slump loss, and what producers can do at the cement, plant, and admixture levels, starting with why cement and admixture compatibility can shift even when the product and the dose stay the same.
What “Hot Cement” Means
Hot cement is portland cement that still carries significant heat when it is loaded and delivered. The heat comes from two places:
- Grinding. Clinker is ground with gypsum in the finish mill, and the friction heats the product. Mills use air and water cooling to limit the rise.
- Storage and dispatch. Cement is a poor heat conductor, so a freshly milled batch shipped quickly, or compacted deep in a silo, can stay hot for a long time.
There is no universal ceiling in ASTM C94 for cement temperature. Industry guidance reports that cement temperatures between roughly 32°C and 77°C are used in concrete during hot weather, and that hot cement may cause loss of slump and perhaps a shorter set time. The same guidance notes that elevated cement temperature adds little else of concern, so the damage is mostly about workability.
Why Fresh-From-Mill Hot Cement Cause Sudden Slump Loss in Concrete
The Sulfate Balance Gets Disturbed
Cement manufacturers grind gypsum into the clinker to slow the very fast reaction of C3A with water. Without it, C3A would stiffen a mix within minutes. The mill is therefore not just grinding, it is also managing a delicate sulfate balance.
Heat changes that balance. In the mill, frictional heat can partly dehydrate gypsum to hemihydrate, and further heating can produce soluble anhydrite, forms of calcium sulfate that dissolve at different rates. One laboratory study on cement storage reports that gypsum dehydration begins near 106°C and is greatest above 125°C. Those are product temperatures inside the mill, not the temperatures you read on a delivery ticket, which is why a hot but not extreme cement can still hide a changed sulfate profile.
False Set: Gypsum Comes Back as Crystals
When a hemihydrate-rich cement meets mixing water, the hemihydrate dissolves quickly and the solution becomes supersaturated. Patent literature describes how the dissolved sulfate then precipitates as gypsum, producing premature stiffening. The mix looks like it has set, but C3A hydration has barely begun. That is why false set often appears within the first few minutes after water contact.
Flash Set: Too Little Soluble Sulfate
The opposite case is flash set, where too little sulfate is available to restrain C3A. An industry discussion on cement milling explains that flash set usually comes from insufficient soluble sulfate, either too little gypsum or gypsum that did not dehydrate enough, and that it is accompanied by abnormal heat release while false set is not. Flash set is the more serious problem.
Heat Goes Straight Into the Concrete
Separate from chemistry, hot cement raises the temperature of the fresh mix, which speeds up hydration and water loss. The effect is real but modest per degree. According to ACI 305, reducing cement temperature by about 8°F (4°C) lowers concrete temperature by only about 1°F (0.5°C). So cooling cement from 75°C to 55°C trims roughly 2.5°C from the concrete. Useful, but it will not explain a truck that stiffens in ten minutes. A sudden loss usually points to the sulfate chemistry, with heat making it worse.
Why PCE Superplasticizers Feel It
Polycarboxylate superplasticizers work by adsorbing on cement particles and holding them apart with side chains. When early dissolution of sulfate changes the ion chemistry of the pore solution, there is more competition for adsorption sites on the reactive aluminate surfaces, and more admixture is consumed early. The practical result is that a PCE dose that held slump for 90 minutes with cool cement may hold it for far less with hot cement. This is also why the same admixture can seem to “stop working” when only the cement lot changed.
False Set vs Flash Set vs Normal Slump Loss
| Feature | False set | Flash set | Normal slump loss |
| Typical timing | First minutes after mixing | Within minutes | Gradual over 30 to 120 minutes |
| Main cause | Hemihydrate or soluble anhydrite rehydrating to gypsum | Not enough soluble sulfate to control C3A | Ongoing hydration, heat, evaporation |
| Heat release | Not abnormal | Abnormal, noticeable | Normal |
| Effect of extended mixing | Often recovers | Usually gets worse | Little recovery |
| First response | Remix, test cement, adjust admixture | Stop and test cement, contact supplier | Slump-retention measures |
An Iowa DOT study summary notes that false set may be overcome by an extended mixing period, while flash set is usually more serious, with workability diminished by extended mixing. That behavior is one of the quickest field clues.
Warning Signs on the Plant and at the Site
- Stiffening appears within minutes of batching, not gradually during haul.
- Several trucks from the same day or the same cement delivery are affected, while earlier deliveries were fine.
- Slump partly returns after extra drum mixing or a short rest.
- The problem worsens on hot afternoons or after a long silo fill.
- Admixture dosage and aggregate moisture records look normal.
- A new cement source, silo, or delivery schedule started recently.
How to Confirm the Cement Is the Cause
Check the cement before changing the mix design:
- Measure cement temperature at the silo discharge or tanker, and log it next to batch records.
- Compare lots. Run the same mix with cement from a different silo or delivery, or with cement that has rested for a few days.
- Run an early stiffening test. ASTM C359 (mortar method), ASTM C451 (paste method), and the mini slump cone test are used to detect early stiffening, though their results can be mixed, so use them as indicators rather than absolute proof.
- Ask the cement supplier for SO3 content, mill exit temperature records, and the gypsum-to-hemihydrate ratio if they measure it.
- Repeat the check on admixture dosage and aggregate moisture to rule out batching error.
Slump loss from low initial moisture or a wrong dose looks different, because the mix is stiff from the start. Hot cement slump loss often follows an acceptable first slump reading.
Practical Controls
| Level | Action | Why it helps |
| Cement supplier | Control mill exit temperature and sulfate dosing, and agree a delivery temperature limit | Prevents gypsum over-dehydration at the source |
| Cement supplier | Rest or rotate silos before dispatch where possible | Lets heat dissipate slowly |
| Concrete plant | Record cement temperature on every delivery | Builds a correlation record |
| Concrete plant | Use chilled water or ice | Offsets heat in the mix |
| Concrete plant | Extend drum mixing for suspected false set | Allows gypsum crystals to break up |
| Admixture | Retune PCE type and dose by trial | Restores dispersion and retention |
Cement Supplier Side
The mill controls the source of the problem. Water spraying and air cooling during grinding limit the temperature, and the sulfate balance is a design decision. Producers should ask suppliers for a written maximum delivery temperature and for notice when the mill or clinker source changes.
Plant Side and Concrete Additive Storage Sensors
Many plants do not monitor cement temperature at all, which makes diagnosis a guessing game. Temperature probes in cement silos, admixture tanks, and water tanks, combined with concrete additive storage sensors that log tank temperature and level, give a time-stamped record. When a stiffening event happens, the log tells you whether cement, water, or admixture temperature changed that day. The same data supports hot-weather admixture adjustments instead of reacting after a rejected load.
Admixture Strategy
A suitable concrete admixture program cannot fix cement that is chemically out of balance, but it can widen the margin:
- Use a slump-retaining PCE or a blend with a fast-dispersing and a slow-release component.
- Consider delayed addition of part of the PCE so that early sulfate chemistry settles before the full dose acts.
- Add a retarder at a low dose for hot, long-haul deliveries.
- Avoid accelerating products on hot-cement days. They push the mix the wrong way, which is a reason to review how the accelerating admixtures market products are specified in hot regions.
- Validate every change in a trial batch with the real cement, at the real temperature, over the full haul time.
Luke Chemicals supplies polycarboxylate superplasticizers and slump-retaining agents, such as VF200 and VF1000, that producers can trial against hot-cement conditions with their own cement.
Why Adding Water Is the Wrong Fix
When a truck stiffens, adding water feels quick. It raises the water-cement ratio, and it can cause bleeding, shrinkage, and higher permeability. For structures that depend on water resistance, this undermines the design. A concrete waterproof admix or a waterproofing admixture for concrete works by densifying the pore structure or blocking capillaries, so concrete that was retempered with extra water starts from a weaker position. The better approach is to control cement temperature, adjust the admixture package, and keep the water content within the approved mix.
Does This Affect Every Type of Concrete?
Not equally.
- Pumped and self-compacting concrete are most exposed, because stiffening raises pump pressure or reduces flow.
- High-strength, low w/c mixes have little free water, so they react quickly to any loss.
- Dry-mix sprayed concrete behaves differently. Cement and aggregate are mixed dry and water is added at the nozzle, so there is no truck-drum slump to lose. Hot cement still matters, though, because it influences how quickly hydration begins at the nozzle, which affects rebound and early set. This is one reason the dry mix sprayed concrete market treats cement temperature as a quality input even though slump is not the headline problem.
Market Context: Why This Problem Is Common in Asia-Pacific
Hot, fast-moving cement supply chains are common where demand is high and climates are warm. Market research notes that Asia-Pacific dominates global PCE consumption, driven by urbanization in India, China, and Southeast Asia, and ready-mix concrete is the largest end-use segment. A separate industry report states that superplasticizers are expected to be the largest type of concrete admixture by value, and that China held the largest share in 2022. That context explains why the APAC concrete admixtures market and the broader concrete admixtures market keep moving toward slump-retaining and hot-climate formulations. The same drivers support growth in the waterproofing admixtures market, where durability specifications are tightening alongside construction volume.
Best Practice Checklist
- Log cement temperature at every delivery or silo transfer.
- Set a written maximum cement temperature with the supplier.
- Rotate silos so freshly milled cement is not used immediately where possible.
- Keep water chilled and aggregates shaded on hot days.
- Run slump checks at several time points for any new cement source.
- Remix suspected false-set loads before judging them.
- Never use water as the default correction.
- Record all admixture adjustments on the batch ticket.
- Revalidate PCE dosage whenever the cement source or mill changes.
Frequently Asked Questions
What temperature is too hot for cement used in concrete?
There is no single limit that applies everywhere. Guidance often cited for hot weather references cement temperatures up to about 77°C, but project specifications and supplier agreements set the real limit. The safer approach is to agree a maximum with your cement supplier and verify with trial batches.
How is false set different from flash set?
False set is a premature stiffening caused by gypsum re-forming from hemihydrate, usually without abnormal heat, and it often improves with more mixing. Flash set comes from too little soluble sulfate and gives off heat, and extra mixing generally does not help.
Does cooling the cement fix the problem?
Partly. Cooling lowers fresh concrete temperature a little, but it does not reverse gypsum that was already dehydrated in the mill. It helps most when heat is the main factor rather than a sulfate imbalance.
Can I add more superplasticizer to restore slump?
Controlled redosing can help if it is approved, trial-tested, and within the manufacturer’s limits. Random additions risk segregation, delayed set, or air content problems.
Why does the same admixture perform differently after a cement change?
Cement chemistry, fineness, C3A reactivity, and sulfate balance all influence how much PCE is adsorbed and how fast it is consumed. A new cement lot, or a hotter one, can change the result without any change in the admixture.
Is hot cement a problem only in summer?
No. Silo compaction and fast dispatch can keep cement hot in any season. Summer simply adds hot aggregates, warm water, and high ambient temperature on top of it.
How do I prove to my supplier that the cement is at fault?
Keep dated temperature logs, run side-by-side batches with cement from different lots, and use an early stiffening test. Reproducible results with one lot and not another are the strongest evidence.